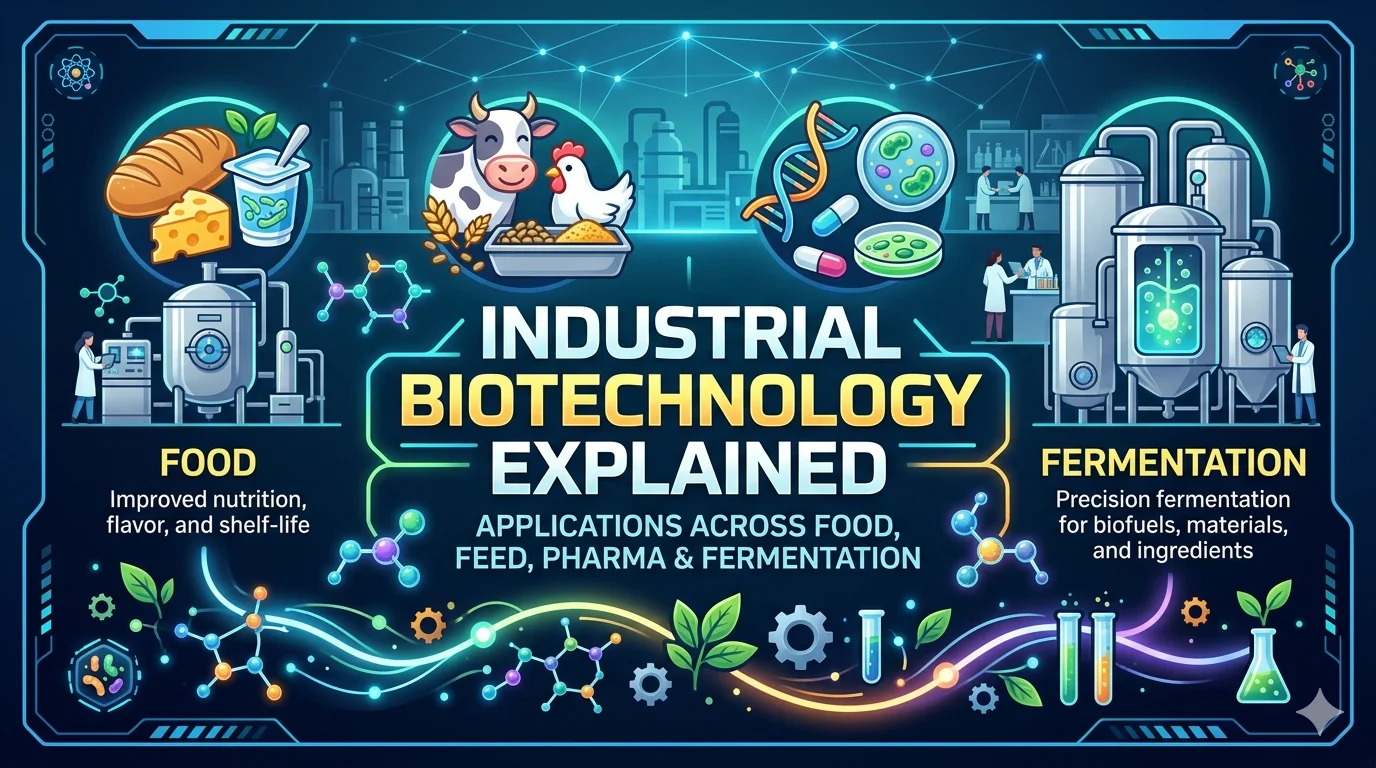
Industrial biotechnology is changing the way manufacturers process raw materials and develop commercial products. By using enzymes, microorganisms and biological systems, industries can improve specific production processes while maintaining product quality. Moreover, these technologies help manufacturers address changing production requirements across different sectors.
Today, industrial biotechnology plays an important role in food processing, animal nutrition and industrial fermentation. For example, enzymes help convert starch into sugars, break down proteins and modify plant fibres. Similarly, microorganisms support fermentation by converting available sugars into useful products.
Leaf CleanTech develops enzyme solutions for food and nutrition, animal feed and fermentation applications. This guide explores the principles of industrial biotechnology, its major applications and the role of industrial enzymes in modern manufacturing.
Key Takeaways
- Industrial biotechnology uses enzymes and microorganisms in manufacturing processes.
- Food processing enzymes support starch conversion, baking, dairy and beverage production.
- Animal feed enzymes help improve nutrient availability and feed ingredient utilisation.
- Fermentation enzymes support starch breakdown and sugar conversion during ethanol production.
- Enzyme selection depends on raw materials, operating conditions and production goals.
What Is Industrial Biotechnology?
Industrial biotechnology uses biological systems, enzymes and microorganisms to manufacture or process commercial products. It is also known as white biotechnology. Unlike conventional processing methods that rely mainly on physical or chemical reactions, this approach uses biological tools to perform specific functions.
For instance, amylase enzymes break down starch into smaller carbohydrate molecules. Meanwhile, proteases act on proteins, and cellulases break down cellulose. These targeted reactions help manufacturers process different raw materials according to their production needs.
Industrial biotechnology has applications across food manufacturing, animal nutrition, grain processing and molasses fermentation. Furthermore, manufacturers can select specialised enzyme systems based on raw material composition and operating conditions.
Why Is Industrial Biotechnology Important?
Manufacturers face increasing pressure to maintain consistent product quality while improving production efficiency. Therefore, industrial biotechnology offers practical ways to optimise selected manufacturing operations through biological reactions.
- Improved processing efficiency: Enzymes accelerate specific reactions under suitable operating conditions.
- Better raw material utilisation: Enzymatic breakdown helps make selected components more accessible during processing.
- Product consistency: Controlled enzyme applications support repeatable processing outcomes.
- Process flexibility: Manufacturers can select enzymes according to their raw materials and production requirements.
- Resource optimisation: Targeted biological processes may help reduce unnecessary processing steps.
- Application-specific solutions: Different enzyme combinations address different industrial challenges.
Role of Enzymes in Industrial Biotechnology
Enzymes are essential tools in industrial biotechnology because each enzyme performs a particular function. Some enzymes break down carbohydrates, while others act on proteins, fats or plant fibres. Consequently, manufacturers select enzymes according to the material they process and the result they want to achieve.
| Enzyme | Primary Function | Industrial Application |
|---|---|---|
| Alpha Amylase | Breaks down starch into smaller dextrins | Starch processing and grain fermentation |
| Glucoamylase | Converts dextrins into glucose | Fermentation and saccharification |
| Protease | Breaks proteins into smaller peptides | Food processing and animal feed |
| Cellulase | Breaks down cellulose | Plant material and food processing |
| Xylanase | Breaks down xylan and related fibre components | Animal feed and grain processing |
| Beta Glucanase | Breaks down beta-glucans | Animal feed and food processing |
| Lipase | Breaks down fats | Food processing and feed applications |
| Phytase | Breaks down phytate and releases bound phosphorus | Animal nutrition |
Industrial Biotechnology Applications in the Food Industry
Food manufacturers use industrial biotechnology to improve processing, ingredient functionality and product consistency. In particular, enzymes support several stages of food production, from raw material preparation to final product development. Moreover, manufacturers can select specialised enzymes to address challenges in different food categories.
1. Starch Processing
Starch is an important raw material in food manufacturing. However, its complex structure often requires enzymatic breakdown before manufacturers can use it in further processing. Initially, alpha amylase breaks starch into smaller dextrins. Subsequently, glucoamylase converts these dextrins into glucose.
These reactions support starch conversion and the production of glucose-rich solutions. Therefore, manufacturers select suitable enzyme systems according to starch sources, processing temperatures and desired conversion levels.
Explore Leaf CleanTech food and nutrition enzymes for application-specific solutions.
2. Baking Industry
Enzymes support several baking applications by modifying dough components and influencing processing characteristics. For example, amylases act on starch, while xylanases modify certain components of wheat flour. In addition, proteases act on proteins and can help adjust dough properties.
As a result, bakeries can select suitable enzyme combinations based on flour quality, dough handling requirements and the characteristics of the finished product. The right formulation also depends on the intended baking process.
3. Dairy Processing
Dairy manufacturers use enzymes to support specific product development and processing needs. Lactase, for instance, breaks lactose into glucose and galactose. This reaction supports the production of lactose-reduced and lactose-free dairy products.
Furthermore, proteases and other specialised enzymes have applications in selected dairy processing operations. The appropriate enzyme depends on the product formulation, processing conditions and required outcome.
4. Fruit and Vegetable Processing
Fruit and vegetable processing often involves managing plant cell structures, pectin and other natural components. Pectinases and cellulases help break down specific structural materials. Consequently, they can support juice extraction, clarification and processing efficiency in suitable applications.
For example, manufacturers may use suitable enzyme preparations to improve the handling of fruit pulp and plant-based materials. However, the exact application depends on the fruit variety and processing objective.
5. Protein Processing
Protein hydrolysis is an important process in food ingredient manufacturing. Proteases break proteins into smaller peptides and amino acids. As a result, manufacturers can use enzymatic hydrolysis to develop protein ingredients with application-specific characteristics.
Moreover, the choice of protease, reaction conditions and processing time influences the final hydrolysate. Therefore, manufacturers should evaluate enzyme performance through suitable application trials.
Industrial Biotechnology Applications in Animal Feed
Animal feed ingredients contain nutrients in different forms. However, some plant-based raw materials also contain fibre components and naturally occurring compounds that can limit nutrient availability. Feed enzymes help break down selected components and support better utilisation of feed ingredients.
Manufacturers include suitable enzymes in feed formulations according to animal species, feed composition and nutritional objectives. In addition, they consider enzyme stability, processing conditions and compatibility with other feed ingredients.
Important Enzymes Used in Animal Feed
| Enzyme | Function | Feed Application |
|---|---|---|
| Phytase | Breaks down phytate and releases bound phosphorus | Plant-based feed formulations |
| Xylanase | Breaks down arabinoxylans and related fibre components | Wheat-based and cereal-based feeds |
| Protease | Breaks proteins into smaller peptides | Protein-rich feed ingredients |
| Cellulase | Breaks down cellulose | Fibre-containing feed ingredients |
| Beta Glucanase | Breaks down beta-glucans | Barley and other cereal-based feeds |
| Mannanase | Breaks down mannan-based polysaccharides | Feed containing mannan-rich ingredients |
| Amylase | Breaks down starch | Starch-containing feed formulations |
Benefits of Feed Enzyme Applications
- Support the breakdown of complex feed components.
- Help improve the availability of selected nutrients.
- Support more efficient utilisation of plant-based ingredients.
- Help feed manufacturers formulate diets around specific raw materials.
- Provide opportunities to optimise feed formulation and processing.
The effectiveness of a feed enzyme depends on its activity, inclusion level, feed composition and processing conditions. Therefore, manufacturers should select products based on application requirements rather than enzyme names alone.
Learn more about animal feed enzyme solutions from Leaf CleanTech.
Industrial Biotechnology in Fermentation
Industrial fermentation uses microorganisms to convert suitable raw materials into valuable products. In grain and molasses fermentation, manufacturers use enzymes and yeast to support the conversion of carbohydrates into fermentable sugars. Subsequently, yeast converts available sugars into fermentation products such as ethanol.
Enzymes play an important role before and during fermentation. First, they help prepare raw materials and break down complex carbohydrates. Then, yeast uses the available fermentable sugars under suitable operating conditions.
1. Grain Fermentation
Grain fermentation typically begins with starch-rich raw materials such as corn and other suitable grains. Since yeast cannot directly ferment intact starch, manufacturers first use enzymes to break it down into simpler sugars.
The process commonly includes two important stages: liquefaction and saccharification. Each stage uses a specific enzyme function to prepare the material for fermentation.
Liquefaction with Alpha Amylase
During liquefaction, high-temperature bacterial alpha amylase (LEAFALFA L) breaks down starch into shorter dextrin chains. This step reduces starch complexity and prepares the material for further conversion.
Moreover, suitable temperature and pH conditions help the enzyme perform effectively. Manufacturers should therefore match enzyme specifications with their process requirements.
Saccharification with Glucoamylase
After liquefaction, glucoamylase converts the resulting dextrins into glucose. Yeast can then use these fermentable sugars during the fermentation stage.
Consequently, effective saccharification helps prepare the carbohydrate source for fermentation. However, the final process performance also depends on raw material quality, enzyme activity and operating conditions.
Yeast and Fermentation Support
Yeast converts fermentable sugars into ethanol and carbon dioxide under suitable fermentation conditions. Meanwhile, manufacturers monitor yeast performance, nutrient availability, temperature, pH and contamination control to manage the fermentation process.
Leaf CleanTech offers grain fermentation solutions, including LEAFALFA L, glucoamylase, LEAFALCO YEAST and BOOSTERZYME. Each product serves a specific role within the fermentation process.
2. Molasses Fermentation
Molasses contains fermentable sugars and other components that make it a useful raw material for industrial fermentation. Nevertheless, its composition can vary depending on the source and processing conditions. Therefore, manufacturers need to manage sugar availability, yeast performance and fermentation conditions carefully.
Enzyme-based solutions can support the utilisation of certain sugar components and help manage specific fermentation challenges. Leaf CleanTech offers specialised products for molasses and cane juice or syrup fermentation applications.
- MOLZYME – An enzyme solution for molasses fermentation applications.
- LEAFFERM J – Designed for cane juice and syrup fermentation applications.
- LEAFFERM F – An enzyme solution for condensate water recycling applications.
- LEAFFERM S – Designed for molasses storage applications.
- LEAFALCO YEAST-M – Active dry yeast for cane sugar molasses fermentation.
These products address different stages and requirements within fermentation operations. For this reason, manufacturers should evaluate the raw material, process conditions and intended application before selecting a suitable solution.
Grain Fermentation vs Molasses Fermentation
| Parameter | Grain Fermentation | Molasses Fermentation |
|---|---|---|
| Primary raw material | Starch-rich grains | Sugar-rich molasses |
| Main carbohydrate | Starch | Sucrose and other sugars |
| Initial enzyme requirement | Alpha amylase for liquefaction | Application-specific fermentation enzymes |
| Further conversion | Glucoamylase for glucose production | Depends on molasses composition and process requirements |
| Fermentation organism | Suitable yeast strains | Suitable yeast strains |
| Important process factors | Starch conversion, temperature and yeast performance | Sugar availability, yeast performance and contamination management |
Industrial Biotechnology and Sustainable Manufacturing
Industrial biotechnology can contribute to more resource-conscious manufacturing by helping companies optimise selected production processes. For example, enzymes perform specific reactions that address processing challenges involving starch, proteins, fats and plant fibres.
In addition, manufacturers can evaluate enzyme-based processes to identify opportunities for improving raw material utilisation and reducing unnecessary processing steps. However, sustainability benefits depend on the complete production system rather than enzyme use alone.
Companies should therefore assess energy consumption, water use, raw material efficiency, enzyme dosage and waste management before making environmental claims. A process-level evaluation provides a more reliable picture of its overall performance.
How to Choose the Right Industrial Enzyme Solution
Selecting an industrial enzyme requires more than identifying the material that needs processing. Manufacturers should evaluate the entire production environment to find a suitable enzyme and application method. The following steps provide a practical starting point.
- Identify the raw material: Understand the composition of the grain, feed ingredient, food material or fermentation substrate.
- Define the processing objective: Determine whether the requirement involves starch conversion, protein hydrolysis, fibre breakdown or fermentation support.
- Check operating conditions: Evaluate temperature, pH, processing time and other relevant conditions.
- Review enzyme activity: Compare enzyme specifications and activity requirements for the intended application.
- Consider process compatibility: Check how the enzyme works with existing equipment, ingredients and processing stages.
- Conduct application trials: Evaluate performance under actual or representative production conditions.
- Work with a suitable manufacturer: Choose an enzyme partner that understands your application and technical requirements.
Industrial Biotechnology vs Traditional Processing
| Comparison | Industrial Biotechnology | Conventional Processing |
|---|---|---|
| Processing approach | Uses enzymes and microorganisms for specific biological reactions | May rely on physical, mechanical or chemical methods |
| Reaction specificity | Enzymes act on specific substrates | Depends on the selected processing method |
| Operating conditions | Depends on enzyme and microorganism requirements | Depends on equipment and process chemistry |
| Applications | Food, feed and fermentation industries | Used across a wide range of manufacturing sectors |
| Process optimisation | Can target specific biological conversion requirements | Can target specific physical or chemical processing requirements |
Industrial Enzyme Solutions from Leaf CleanTech
Leaf CleanTech is an industrial biotechnology and enzyme solutions company focused on food and nutrition, animal feed and fermentation applications. The company develops enzyme products to address different processing requirements across these sectors.
Its portfolio includes specialised enzymes and formulations for carbohydrate conversion, protein processing, fibre breakdown and fermentation applications. Furthermore, Leaf CleanTech offers solutions for grain and molasses fermentation, helping manufacturers explore application-specific enzyme technologies.
Explore Leaf CleanTech Product Categories
- Food and Nutrition Enzymes – Enzyme solutions for food processing and ingredient applications.
- Animal Feed Enzymes – Enzymes for feed ingredient processing and animal nutrition applications.
- Fermentation Products – Enzyme and yeast solutions for grain and molasses fermentation.
To learn more about the company's biotechnology expertise and product development approach, visit About Leaf CleanTech. Alternatively, explore the product categories to find solutions relevant to your manufacturing requirements.
Future of Industrial Biotechnology
Industrial biotechnology continues to develop as manufacturers look for specialised solutions to meet changing production requirements. Advances in enzyme engineering, microbial technology and process optimisation are creating opportunities across food manufacturing, animal nutrition and fermentation.
Moreover, manufacturers increasingly focus on application-specific enzyme systems rather than relying on general-purpose processing methods. This approach allows companies to evaluate raw materials, operating conditions and desired outcomes together.
As the industry develops, enzyme manufacturers and industrial processors will continue to work together to improve biological conversion processes. Consequently, industrial biotechnology will remain an important area of innovation for manufacturers seeking suitable process improvements.
Frequently Asked Questions About Industrial Biotechnology
1. What is industrial biotechnology?
Industrial biotechnology uses enzymes, microorganisms and biological processes to manufacture or process commercial products. It has applications in food processing, animal feed and industrial fermentation.
2. What are the main applications of industrial biotechnology?
Major applications include food processing, starch conversion, baking, dairy production, animal feed manufacturing, grain fermentation and molasses fermentation. Each application uses specific biological processes to address production requirements.
3. What is the role of enzymes in industrial biotechnology?
Enzymes act as biological catalysts. They help break down or convert specific materials such as starch, proteins, fats and plant fibres during industrial processing. Therefore, manufacturers select enzymes according to their processing objectives.
4. Which enzymes are commonly used in food processing?
Common food processing enzymes include amylase, glucoamylase, protease, cellulase, hemicellulase, xylanase, pectinase, lactase and lipase. However, the appropriate enzyme depends on the food application and processing conditions.
5. How does industrial biotechnology help the animal feed industry?
Feed enzymes help break down selected feed components, including phytate, fibre, proteins and starch. As a result, they can support nutrient availability and feed ingredient utilisation.
6. What is the role of phytase in animal feed?
Phytase breaks down phytate, a compound found in many plant-based feed ingredients. This process releases some of the phosphorus bound within phytate, making it more available.
7. What is grain fermentation?
Grain fermentation uses starch-rich grains as raw materials. First, enzymes convert starch into fermentable sugars. Then, yeast converts those sugars into fermentation products such as ethanol.
8. Why are alpha amylase and glucoamylase used in grain fermentation?
Alpha amylase breaks starch into smaller dextrins during liquefaction. Subsequently, glucoamylase converts these dextrins into glucose during saccharification, providing fermentable sugars for yeast.
9. What is molasses fermentation?
Molasses fermentation uses sugar-rich molasses as a raw material. Suitable yeast converts fermentable sugars into products such as ethanol under controlled process conditions.
10. How do manufacturers select industrial enzymes?
Manufacturers should consider raw material composition, enzyme activity, temperature, pH, processing time, compatibility and the desired production outcome before selecting an enzyme. Application trials can also help assess suitability.
11. What is white biotechnology?
White biotechnology is another name for industrial biotechnology. It refers to the use of biological systems, enzymes and microorganisms in industrial production and processing.
12. Where can manufacturers find industrial enzyme solutions in India?
Manufacturers can explore specialised enzyme suppliers based on their application, technical requirements and product specifications. Leaf CleanTech provides enzyme solutions for food and nutrition, animal feed and fermentation applications.
Conclusion
Industrial biotechnology is an important part of modern manufacturing. By using enzymes and microorganisms, industries can improve specific processing operations across food production, animal nutrition and industrial fermentation.
From starch conversion and protein hydrolysis to feed enzyme applications and ethanol fermentation, biological solutions support a wide range of industrial requirements. However, successful implementation depends on choosing the right enzyme, understanding the raw material and maintaining suitable process conditions.
Leaf CleanTech offers specialised enzyme solutions for food and nutrition, animal feed and fermentation. Explore its product range to identify solutions that match your manufacturing requirements.
Looking for Industrial Enzyme Solutions?
Discover enzyme solutions for food processing, animal feed and industrial fermentation with Leaf CleanTech. Connect with the team to discuss your application and technical requirements.
Contact Leaf CleanTech
Animal Feed Enzymes Guide: Types, Uses & Benefits - Leaf CleanTech
April 4, 2026[…] The appropriate enzyme depends on the feed substrate, processing conditions and intended nutritional application. For additional background on enzyme applications, visit Leaf CleanTech's industrial biotechnology applications guide. […]