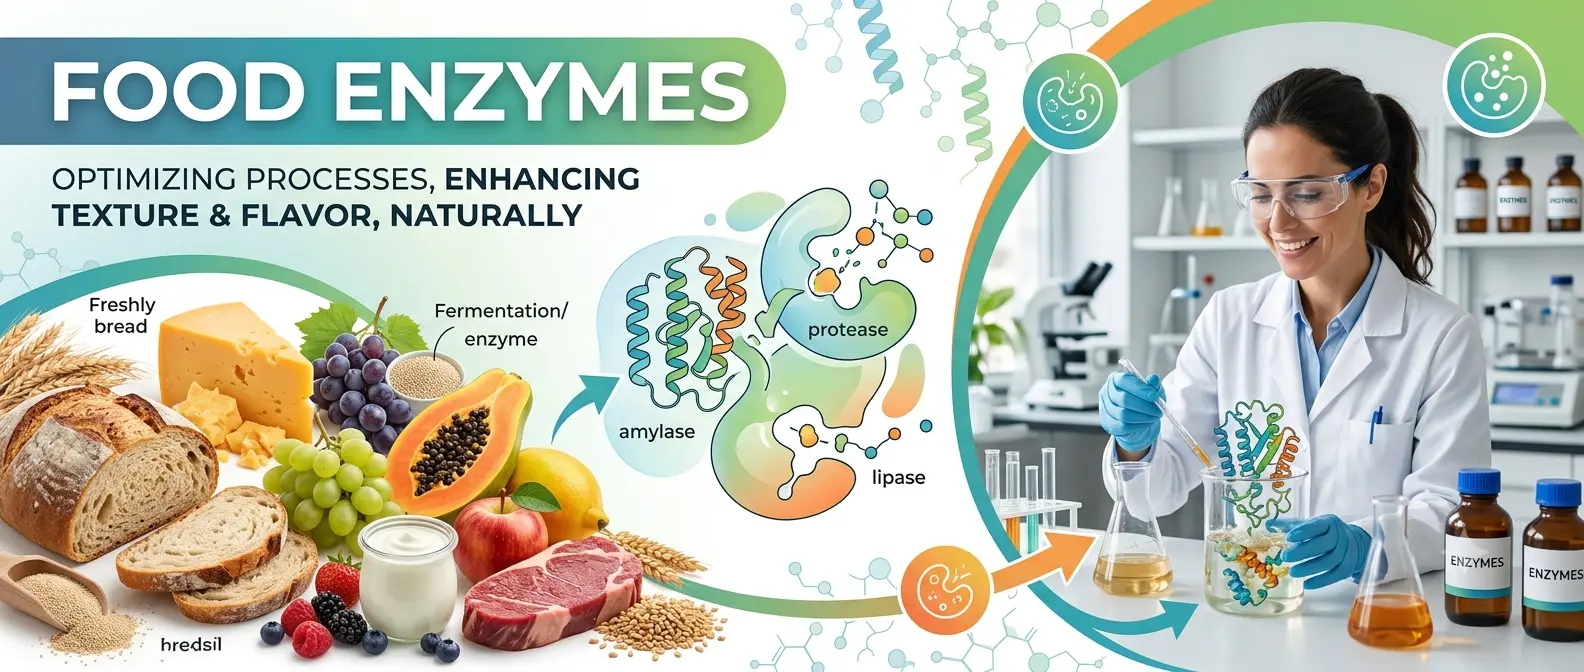
Food enzymes are an important part of modern food processing. They help manufacturers control specific biochemical reactions involving proteins, carbohydrates, fibres, fats and sugars. By targeting these components, enzymes can support better processing efficiency, product consistency, texture, yield and overall product quality.
From baking and dairy processing to beverages, fruit processing, confectionery, starch conversion and protein hydrolysis, food processing enzymes are used across a wide range of manufacturing applications.
Leaf CleanTech develops and manufactures food enzyme solutions designed around different processing requirements, including standard enzyme products and customised formulations.
Food enzymes are biological catalysts that accelerate specific chemical reactions. They work by acting on particular substrates such as starch, protein, lactose, cellulose, pectin and fats.
In food manufacturing, the right enzyme can help modify a raw material or intermediate product under controlled processing conditions.
For example:
The choice of enzyme depends on the raw material, target reaction, processing conditions and desired final-product characteristics.
Food manufacturers use enzymes because they can provide targeted biological activity during processing.
Depending on the application, food enzymes can support:
Enzymes can accelerate specific reactions and help manufacturers manage processing steps more efficiently.
For example, amylases can support starch breakdown, while pectinases can assist with fruit pulp treatment and clarification.
Controlled enzymatic activity can help manufacturers achieve more consistent processing results from batch to batch.
This is particularly important in applications such as baking, beverage processing, dairy production and starch processing.
Certain enzymes can modify proteins, starches, fibres or fats to achieve desired product characteristics.
Proteases, amylases and lipases, for example, can be used in different food applications where controlled modification of raw materials is required.
Enzymes that act on plant cell-wall components can help improve processing of fruits, vegetables and other plant-based materials.
Pectinase, cellulase and hemicellulase can be used to support pulp treatment, viscosity management and extraction processes.
Proteases, lactase, glucoamylase and other hydrolytic enzymes help break larger molecules into smaller components.
This makes them useful in applications involving protein hydrolysis, lactose reduction and starch conversion.
Different enzymes perform different functions. Understanding the target substrate is one of the first steps in selecting an appropriate food enzyme.
Proteases are enzymes that hydrolyse proteins into smaller peptides and amino acids.
They are used in applications where controlled protein breakdown is required, including protein processing, baking, dairy applications and selected beverage processes.
Leaf CleanTech offers both acid protease and neutral protease solutions for different processing conditions.
Related enzyme solutions:
Proteases are particularly useful when manufacturers need to control the degree of protein hydrolysis or modify protein functionality.
Amylases act on starch and are widely used in food processing.
They can support starch liquefaction, dextrinisation and the conversion of complex carbohydrates into smaller molecules.
Fungal alpha amylase is commonly used for controlled starch modification, while glucoamylase can further hydrolyse dextrins to glucose.
Related enzyme solutions:
These enzymes can be relevant to baking, starch processing, brewing, fermentation and other carbohydrate-processing applications.
Pectinase enzymes act on pectin, a structural polysaccharide found in fruits and vegetables.
They are particularly relevant to fruit and vegetable processing, where excessive viscosity or suspended material can affect processing and clarification.
Leaf CleanTech's pectinase formulation is designed for applications involving fruit and vegetable pulps and purees, including viscosity reduction.
Related product:
[Pectinase Enzyme Powder]
Pectinase can therefore support applications such as:
Cellulase breaks down cellulose, which is an important structural component of plant cell walls.
In food processing, cellulase can help improve the breakdown of plant-based materials and support processing of fibrous raw materials.
Related product:
[Food Grade Cellulase Enzyme]
Cellulase may be used alongside other fibre-degrading enzymes depending on the raw material and process objective.
Hemicellulase and xylanase target components of plant cell walls and hemicellulose.
They can be useful in grain, cereal, baking and other plant-based processing applications.
Related products:
Xylanase specifically acts on xylan-containing substrates and can support controlled hydrolysis of hemicellulosic components.
Beta glucanase helps hydrolyse beta-glucans into smaller molecules.
Beta-glucans can contribute to viscosity in certain cereal-based processing systems. Enzymatic hydrolysis can therefore be useful where viscosity management is an important processing objective.
Related product:
[Beta Glucanase Enzyme Powder]
Lactase, also known as beta-galactosidase, hydrolyses lactose into glucose and galactose.
This makes lactase particularly relevant to dairy processing and the development of lactose-reduced or lactose-free dairy products.
Related product:
[Lactase Enzyme Powder]
Leaf CleanTech's lactase solution is produced through controlled fermentation and is intended for applications where controlled lactose hydrolysis is required.
Lipase acts on fats and lipids.
In food processing, lipases can support controlled fat hydrolysis and are used in selected applications involving dairy, bakery and other food products.
Related product:
[Lipase Enzyme Powder]
The specific function of lipase depends on the food matrix, processing conditions and desired product characteristics.
Invertase catalyses the hydrolysis of sucrose into glucose and fructose, producing invert sugar.
This makes invertase useful in selected confectionery and food-processing applications where control of sugar crystallisation, texture and sweetness characteristics is required.
Related product:
[Invertase Enzyme Powder]
Leaf CleanTech's LEAFINVERT is produced from yeast through controlled fermentation, isolation and ultrafiltration.
Alpha-galactosidase breaks down certain complex carbohydrates, including raffinose and stachyose.
It can be useful when processing plant-based ingredients containing these carbohydrate components.
Related product:
[Alpha Galactosidase Enzyme]
Papain is a proteolytic enzyme obtained from papaya.
It can be used to modify proteins in food-processing applications. Leaf CleanTech's papain solution is particularly positioned for biscuit manufacturing, where it can support dough characteristics, biscuit volume, texture and freshness.
Related product:
[Papain Food Enzyme]
Bromelain is a group of proteolytic enzymes associated with pineapple.
It can be used in food and nutrition applications requiring proteolytic activity.
Related product:
[Bromelain Enzyme Powder]
Food enzymes are not limited to one type of product. Their applications extend across multiple food-processing sectors.
Enzymes can support dough handling, starch modification, texture, volume and product freshness.
Amylases, proteases, xylanases and other enzyme systems can be selected according to the formulation and desired product characteristics.
Dairy manufacturers use enzymes for specific processing requirements.
For example, lactase can hydrolyse lactose, while lipase can support controlled modification of milk fat in selected applications.
Enzymes can support clarification, viscosity management and conversion of specific components in beverage production.
Pectinase is particularly relevant to fruit juice and beverage processing.
Fruit and vegetable processing often involves pectin, cellulose and other plant-wall components.
Pectinase, cellulase and hemicellulase can therefore support pulp treatment, extraction, viscosity reduction and clarification.
Invertase can convert sucrose into glucose and fructose, producing invert sugar for selected confectionery applications.
Amylases, glucoamylase, beta glucanase and proteases can support starch conversion and processing efficiency in brewing and fermentation systems.
For industrial fermentation applications, explore Leaf CleanTech's [Fermentation Solutions] as a related area.
Proteases can hydrolyse proteins into smaller peptides and amino acids.
This makes them relevant to protein hydrolysates, nutritional ingredients and other food-processing applications requiring controlled protein modification.
Selecting an enzyme is not simply a matter of choosing the most powerful enzyme.
The enzyme needs to match the process.
Important factors include:
1. Substrate:
What material will the enzyme act on?
2. Target reaction:
What specific reaction or modification is required?
3. pH:
At what pH does the process operate?
4. Temperature:
What is the processing temperature and how long will the enzyme remain active?
5. Reaction time:
How long is the enzyme expected to act?
6. Dosage:
What enzyme activity is required for the intended result?
7. Final product requirements:
Is the objective improved texture, viscosity reduction, hydrolysis, clarification, extraction or another processing characteristic?
For this reason, application-specific enzyme selection is important for achieving predictable results.
Not every production process has identical requirements.
A standard enzyme can be suitable for many applications. However, some manufacturers work with unusual raw materials, processing conditions or multiple substrates.
In these situations, a customised food enzyme formulation can combine complementary enzyme activities around a specific processing requirement.
Leaf CleanTech develops customised enzyme formulations for food-processing applications where standard enzyme solutions may not provide the required combination of activities.
Related service:
[Customised & Formulated Food Enzymes]
Leaf CleanTech combines biotechnology expertise with application-focused enzyme development.
Its food and nutrition portfolio includes proteases, amylases, cellulases, hemicellulases, xylanases, pectinases, lactase, lipase, invertase, bromelain, papain and customised enzyme formulations.
Enzyme selection is based on the customer's raw material, processing conditions and desired outcome.
Food enzyme solutions are developed with a focus on consistent enzyme activity and reliable processing performance.
Where a standard enzyme does not meet a specific requirement, customised enzyme blends can be developed.
Leaf CleanTech works with manufacturers to identify suitable enzyme activities and optimise their application.
The company is based in Bengaluru, India, and develops enzyme solutions for Food & Nutrition, Animal Feed and Fermentation applications.
Food enzymes are biological catalysts used in food processing to modify or break down specific components such as proteins, starches, sugars, fibres and fats.
Common food-processing enzymes include proteases, amylases, glucoamylase, pectinase, cellulase, xylanase, hemicellulase, lactase, lipase, invertase, alpha-galactosidase, bromelain and papain.
Food enzymes are used for applications including baking, dairy processing, beverage production, fruit and vegetable processing, starch conversion, confectionery, brewing, fermentation and protein hydrolysis.
Selection depends on the substrate, target reaction, pH, temperature, reaction time, enzyme activity and desired final-product characteristics. Application-specific technical evaluation can help identify a suitable enzyme.
Yes. Custom enzyme formulations can combine different enzyme activities to address specific raw materials, processing conditions or production objectives.
Food-grade enzymes are specifically developed for controlled applications in food manufacturing. The appropriate enzyme and formulation depend on the intended process and applicable food-safety requirements.
Protease acts on proteins, while amylase acts primarily on starch. They therefore perform different functions in food-processing applications.
Pectinase breaks down pectin and can support fruit and vegetable processing, including pulp treatment, viscosity reduction, extraction and juice clarification.
Every food-processing application has different requirements. The right enzyme depends on your raw material, process conditions and desired result.
Share your application, substrate and processing conditions with Leaf CleanTech's technical team to identify a suitable food enzyme solution.
[Explore Food & Nutrition Enzymes] | [Request a Custom Enzyme Solution] | [Contact Leaf CleanTech]
[…] CleanTech also provides a broader range of food and nutrition enzymes for applications across food processing and […]
©2026. Leaf CleanTech - All Rights Reserved.
Customised Food Enzyme Formulations - Leaf CleanTech
May 5, 2026[…] For the complete picture of our enzyme categories, visit the food enzymes guide. […]